If you’ve ever walked into a hardware store and grabbed a sturdy door hinge, a durable window latch, or a rust-resistant fence bracket, there’s a good chance it started life in a construction hardware die casting mold. For the last 12 years, I’ve run a small mold shop that specializes in building exactly those tools—we don’t mess with consumer trinkets or tiny electronic parts. We build big, heavy-duty molds for parts that hold up buildings and communities, so I’ve seen every risk that comes with investing in this niche. I’m not here to sell you a bill of goods (not this time, anyway); I’m here to tell you the real, gritty risks you need to know before you drop six or seven figures on a mold, and maybe how to dodge some of them. Construction Hardware Die Casting Mold
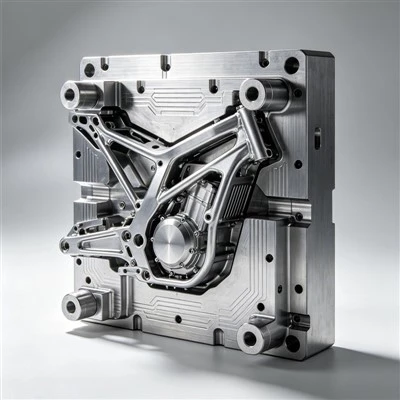
First, let’s get one thing straight: construction hardware die casting isn’t like making plastic toys or phone cases. The parts we produce have to hold up to extreme weather—freeze-thaw cycles, salt air, direct sunlight, even being slammed by a screen door or a sledgehammer. That means the molds that make them have to withstand massive heat, pressure, and repetitive use. Skip a step, and your mold will fail before you make 10,000 good parts.
The biggest risk I see every single day is material mismatch. Let me break it down. A customer comes to me with a quote, says “I need zinc molds for 20,000 door handles.” They show me a CAD file, give me a budget, and that’s it. I ask “What grade of zinc are you using?” and they stare at me like I just asked them to solve quantum physics. Most of the time, they picked the cheapest zinc alloy they could find online—something with a high lead content, because it’s super cheap. But here’s the catch: that cheap zinc softens way too fast when you’re injecting it at 700 degrees into a steel mold. The mold’s steel will erode in weeks, not years, and those soft spots will make every other part you produce warped or pitted. I had a customer last year who skipped that question, went with the cheapest zinc, and had to scrap his entire $80k mold job 3 months in because the cavity walls were so worn they couldn’t make a latch that fit a standard 1/4 inch screw. He didn’t just lose the mold cost—he lost 10,000 parts that were useless, and he had to pay for rework on his assembly line. That’s the kind of hidden risk no one talks about until it bites.
Then there’s the mold design flaw that’s not obvious on paper. Everyone uses CAD now, right? You drag and drop shapes, click a button, and get a perfect digital model. But CAD can’t account for what happens when you inject molten metal at 10,000 PSI into a mold that’s 3 feet long and 2 feet wide. I’ve seen customers design a mold for a 12-inch gate hinge with a super sharp corner to save material, but that corner became a stress point that cracked the mold after 500 cycles. Another time, a client forgot to add ejector pin clearance for a window sash part—so every time the mold closed, the pin bent and scraped the inside of the cavity, leaving a scratch on every part. These aren’t “oops” mistakes; they’re design shortcuts that sound smart in theory but destroy your investment. The worst part? Most mold shops will quote you a fast turnaround and cut corners on design to hit that deadline. I always tell customers: if a shop offers a 2-week turn on a 3-foot, multi-cavity construction mold, run. Good design takes 4 weeks minimum, and it’s where you avoid the big risks.
Next up, manufacturing and workmanship that looks fine until it’s not. Let’s be real—most mold builders outsource at least part of the job, or use entry-level CNC machines to cut steel. I’ve seen a mold that was milled on a $50k CNC, not a $200k high-precision one, so the cavity walls were off by 0.002 inches. That’s not a big number on paper, but when you’re trying to make a door latch that has to fit tight and not wiggle, 0.002 inches is the difference between a part that passes inspection and one that gets rejected. Even smaller shops like mine have had to fix work from subcontracted tool makers who rushed through the surface finishing—they left micro-pits in the mold cavity that leave tiny bubbles on every part, making them look cheap and corrode faster. A customer of mine who makes commercial door handles once bought a mold from a shop that used a low-grade tool steel for the core pins. Those pins bent within 1,000 cycles, and because they were hidden inside the hinge’s barrel, no one noticed until the parts were already on the assembly line. That cost him $15,000 in scrap, plus a week of downtime.
Then there’s the hidden post-investment cost, aka the “we forgot to tell you this part” risk. You buy the mold, pay for shipping, and start producing parts. But wait—you need specialized cooling lines to keep the mold from overheating, right? Construction molds run nonstop, 24/7, because if you stop, the metal in the cavity freezes and you have to break the mold open. Most cheap mold builders skip adding enough cooling lines to save a few bucks, so you end up having to pay $5k-$10k to have them retrofitted, which delays production for weeks. Or they don’t include the proper venting—so when you inject molten metal, air gets trapped in tight corners, leaving voids in the part that make it weak enough to break under normal use. I had a residential fence manufacturer come to me last year because the mold he bought had bad venting. His fence brackets were cracking when he hammered them into posts, and his customers were sending them back. We had to re-machine the vents, and he lost $20k in warranty claims before he fixed it. That’s the worst risk because it’s not up front—it creeps up on you when you’re already invested.
Wait, let’s not forget about supply chain chaos that hits right when you need your mold. A lot of mold shops use pre-cut steel blocks from overseas, right? I’m in the US, and even we sometimes source high-grade P20 steel from a mill in Taiwan. If there’s a shipping delay, or a steel mill strike, or even a global shortage of certain metal grades, your mold order gets pushed back 3 months. I had a customer last year who ordered a mold in March 2022, right when the war in Ukraine started, and his steel block was stuck in a port in Rotterdam for 6 weeks. He was supposed to launch a new line of commercial window parts in June, and he missed the summer construction season entirely. That cost him over $100k in lost contracts, just because a steel shipment got held up. No one tells you that investing in a construction mold isn’t just about the mold—it’s about getting the materials on time too.
And let’s talk about the skill gap. A lot of new mold builders popped up during the pandemic when demand for construction parts spiked. They were guys who knew how to run a CNC, but not how to design a mold that could handle 10,000 cycles of heavy, molten metal. When I started, my mentor told me that a good mold maker isn’t just someone who can cut steel—they understand heat transfer, metal flow, stress points, and what it takes for a part to last 20 years in the sun or snow. Most of those new shops don’t have that institutional knowledge. I’ve fixed molds from guys who’d never built a construction die casting mold before, and half the time, the original maker didn’t even have a background in construction hardware—they just used a generic mold design they found online. That’s a disaster waiting to happen, because construction parts aren’t consumer stuff—they have load requirements, corrosion standards, and code needs that generic molds can’t meet.
So, what do you do if you’re investing in this kind of mold? For what it’s worth, here’s the stuff I tell every customer who walks through my door. First, don’t chase the cheapest quote. If a mold is 30% lower than everyone else’s, there’s a reason—they’re cutting corners on steel grade, design, or cooling lines. Ask specific questions: “What grade of tool steel are you using for the cavity?” “How many cooling lines are there, and where are they placed?” “Have you built a mold for this exact part before?” Second, if you can, ask for a test sample. A good mold shop will run 50-100 test cycles before sending you the mold, so you can check the part quality. If a shop refuses that, run. Third, look for a shop that offers local support—if something breaks, you don’t want to wait 2 weeks for a tech to fly in. I’m based in Ohio, so I can drive to a customer’s factory in Michigan or Pennsylvania the same day if there’s an emergency.

At the end of the day, investing in a construction hardware die casting mold is a big bet—you’re looking at six figures, months of lead time, and your brand’s reputation. I’ve seen guys win big by picking the right mold, and I’ve seen guys lose their entire business because they skipped the fine print. I’ve built molds that have lasted 10 years, running nonstop, and I’ve fixed molds that should’ve been scrapped before they left the shop. If you’re ready to stop guessing and work with someone who knows the ins and outs of construction hardware molds—no sales fluff, no hidden fine print—reach out. We can talk through your part, your timeline, and make sure you avoid the risks that sink so many new projects.
Zinc Alloy Die Casting Mold References:
- Die Casting Mold Design Handbook, 2nd Edition, Society of Manufacturing Engineers, 2021
- Construction Hardware Performance Standards, ASTM International, F845-20
- Tool Steel Selection for Die Casting Applications, Association of Die Casting Engineers, 2022
Hangzhou Pullbull Technology Co., Ltd.
As one of the most professional construction hardware die casting mold manufacturers and suppliers in China, we offer a wide range of products with superior quality. Please feel free to wholesale bulk premium construction hardware die casting mold from our factory. Also, custom service is available.
Address: Rm 805 Gemini Build 1, #1785 JiangHan Rd, BinJiang, Hangzhou, China 310052
E-mail: markdan@menovo.cn
WebSite: https://www.pbmold.com/
